
CIT-25 Application Guide

1. PRODUCT INFORMATION
1.1 Product description:
CIT-25 is a light-curable polymer-based resin designed for the fabrication of biocompatible, transient use, removable dental appliances by 3D printing. It is intended for 3D printing of custom impression trays.
1.2 Intended use:
CIT-25 resin is a light-curable polymer-based resin designed for the fabrication of biocompatible, transient use, removable dental appliances by 3D printing. It is intended for 3D printing dental accessories such as dental impression trays.
1.3 Material associated warnings:
CIT-25 in its uncured state contains monomers that polymerize during 3D printing. Please read MSDS of CIT-25 material which is available at https://ameralabs.com/msds/ for hazards associated with liquid material.
The uncured liquid resin is not safe for contact with food, drinks, or the human body. In its liquid, uncured state, this resin is a hazardous chemical. Use protective gloves and glasses at all times when handling it. Provide adequate ventilation. Store resin at room temperature away from direct sunlight. Resins are classified as dangerous chemicals and must be disposed of properly in designated containers. Resin bottles, empty or full, must never be disposed of or poured into general waste.
2. REQUIREMENTS
2.1 Hardware
2.1.1 3D printer
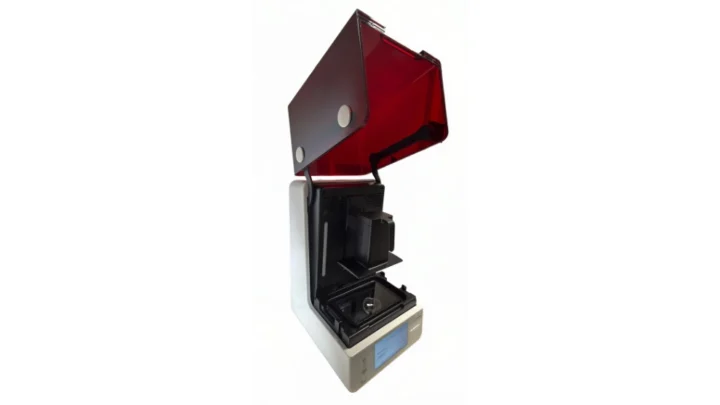
In order to print with CIT-25 3D printing material for custom impression tray models, you need LCD/mSLA or DLP 3D printer with the light source of 385nm or 405nm. If your machine has recommended settings on our website, they should be a good starting point and fine-tuned according to your environment if needed. Usually, each machine and work environment is relatively unique, thus, some minor adjustments to printing settings may be needed. We keep 3D printing settings up to date on our website.
2.1.2 Resin tray and build platform
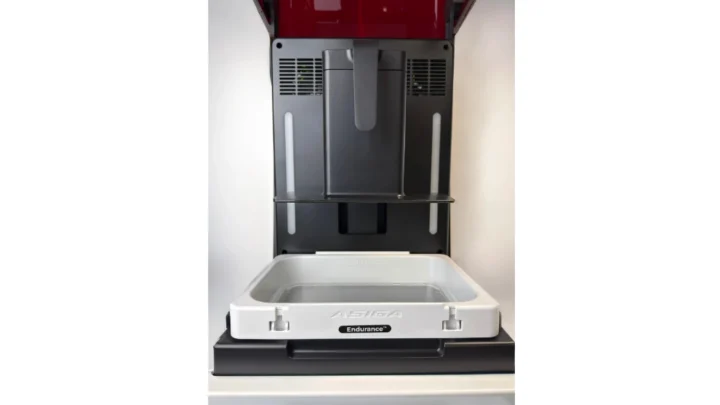
You also need a separate resin tank and build platform to ensure biocompatibility for products made with CIT-25 resin. In general, you should always use a separate resin tray and build platform for biocompatible resins. If resin is mixed with another material, biocompatibility could be compromised.
2.1.3 Washing equipment
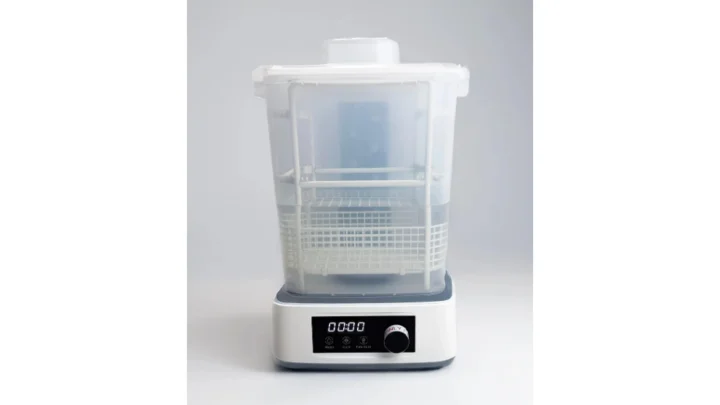
Regular washing station with magnetic stirring could be used. However, regular sealed containers could be used as well. It is important that the washing station is dedicated to biocompatible materials as using one washing station with other non-biocompatible resins will compromise biocompatibility.
2.1.4 Post-curing equipment
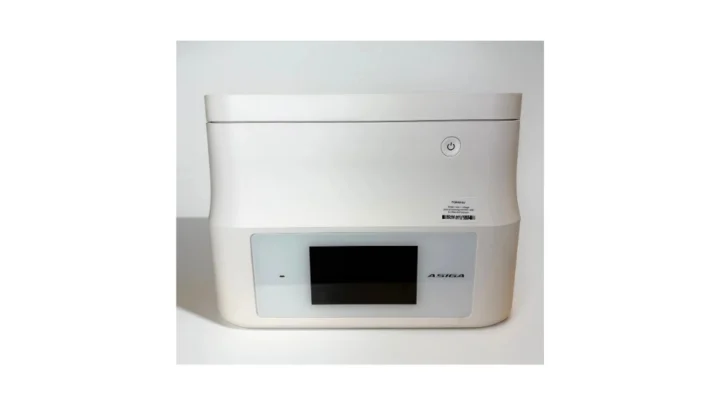
General post-curing equipment with 385nm, 395nm or/and 405nm light sources could be used.
2.2 Software
We do not have strict requirements for 3D printing software as it depends on your 3D printer. You could use any software you like as long as it fulfils your requirements and works best for you. In this usage guide we will be using Asiga Composer.
2.3 Materials
Apart from CIT-25 material for 3D printing, you will also need 99 % isopropyl alcohol (IPA) used for cleaning manufactured objects.
2.4 Safety equipment
In order to work safely, protective eyewear, nitrile gloves and laboratory clothing are required. Moreover, air ventilation is mandatory in the room with at least 4 times/hour air exchange. Otherwise do your work, including 3D printing, in the fume hood.
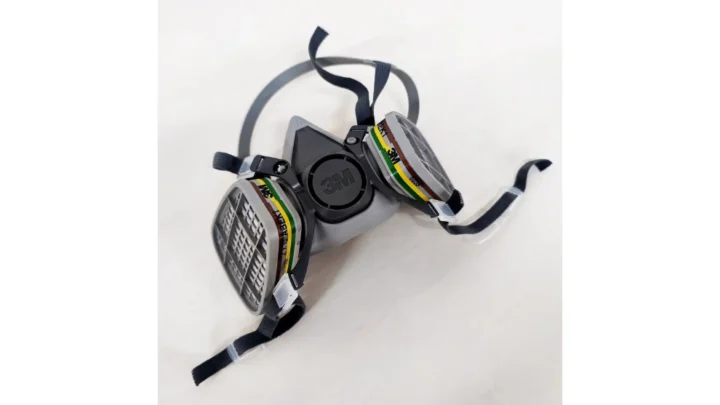
We also do recommend wearing half facepiece reusable respirator with gas and vapor filters.
3. CUSTOM IMPRESSION TRAY DESIGN
3.1 Recommended design parameters
The design of the custom impression tray model may vary case-by-case and depending on the software package you use. Nonetheless, adjust design settings thoroughly and carefully to ensure precision, comfort and, most importantly, safety. We have prepared general guidelines that could be followed when designing custom impression tray models. Modify these design settings according to your situation and experience.
| Parameter | Recommendation |
| Wall thickness | We recommend setting it to at least 3 mm. Walls that are too thin could result in structural instabilities and weaker structures. However, too thick a wall could cause printing issues due to too large cross-sectional area and loss of precision due to higher material shrinkage. |
| Handle thickness | We recommend setting it to at least 4 mm. This is to ensure it does not break while removing the tray from the patient’s mouth. |
| Retention holes | We recommend adding holes at least 2 mm in diameter. Retention holes will help with impression material adhesion to the custom impression tray. However, they should be spaced at least 5 mm to ensure sufficient strength of the printed tray. |
| Handle shape | We recommend the handle to be molded into the model. Sharp corners might cause stress points which can lead to breaking of the handle which complicates removal of the impression tray from the patient’s mouth. So, an even transition between the model and the handle is preferred. |
The exact step-by-step design varies by software package. For detailed advice on designing impression tray models, contact your software manufacturer.
4. 3D PRINTING
4.1 Defining printing parameters
Before importing actual 3D model into the software, we highly recommend setting up your software with appropriate 3D printing parameters, such as exposure times, lifting distances and various speeds.
For the first print using this material, it is advised to print something small first. We recommend the AmeraLabs Town calibration model.
These parameters highly depend on the machine being used. The list of validated 3D printers and corresponding parameters can be found on our website.
NOTE: The list of 3D printers on our website is not definitive. It represents our tested and validated set of machines. It is possible to use other 3D printers as long as correct exposure and other settings are obtained. Feel free to contact us if you need help determining correct 3D printing parameters.
4.2 Importing models
Open software package of your choice and import *.STL (or *.OBJ if supported) file.
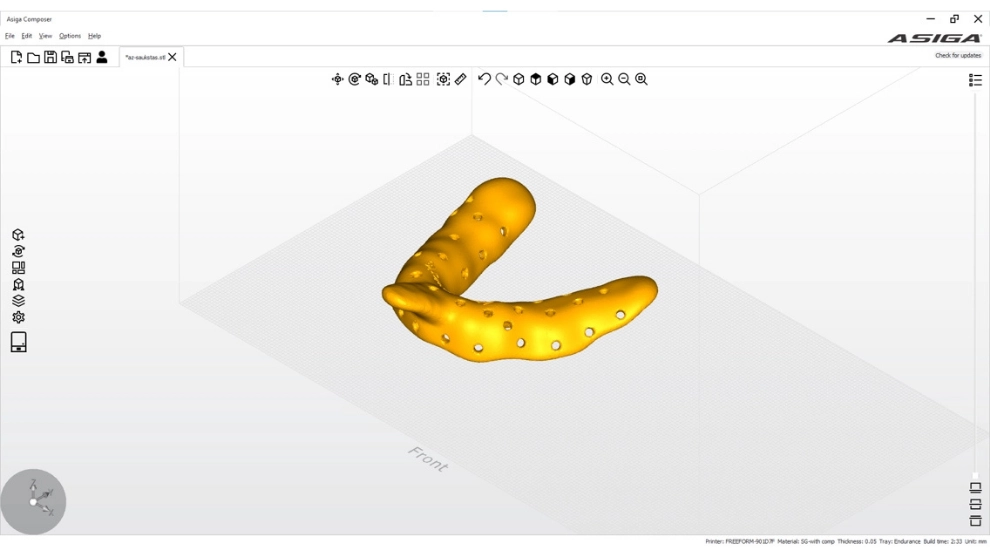
4.3 Orient your model
Position custom impression tray model at a slight angle.
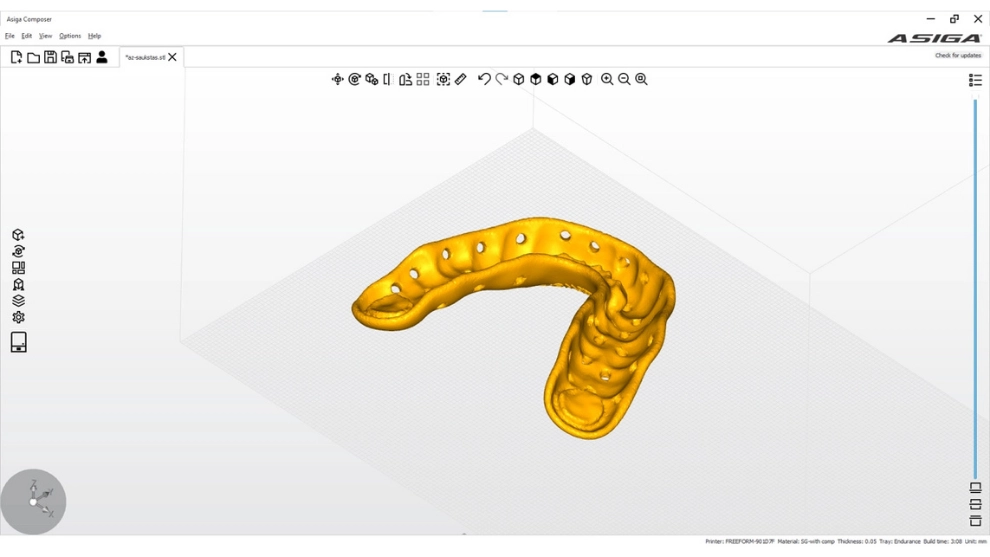
The impression tray model should be oriented so that all supports are placed on the surface which will not be in contact with the impression material. This will reduce the amount of post-processing while ensuring the best accuracy. The only exception would be if impression tray models are used that do not have retention holes which would lead to potential formation of suction cup areas. This would require changing orientation so that no closed volumes form and allow air and resin flow freely.
4.4 Generate support structures
You can set up support structures based on the following table.
| Parameter | Value |
| Strut diameter, mm | 0.8 |
| Tip diameter, mm | 0.3 |
| Tip depth, mm | 0.1 |
| Density/Spacing, mm | High/2 |
| Raft thickness, mm | 0.2 |
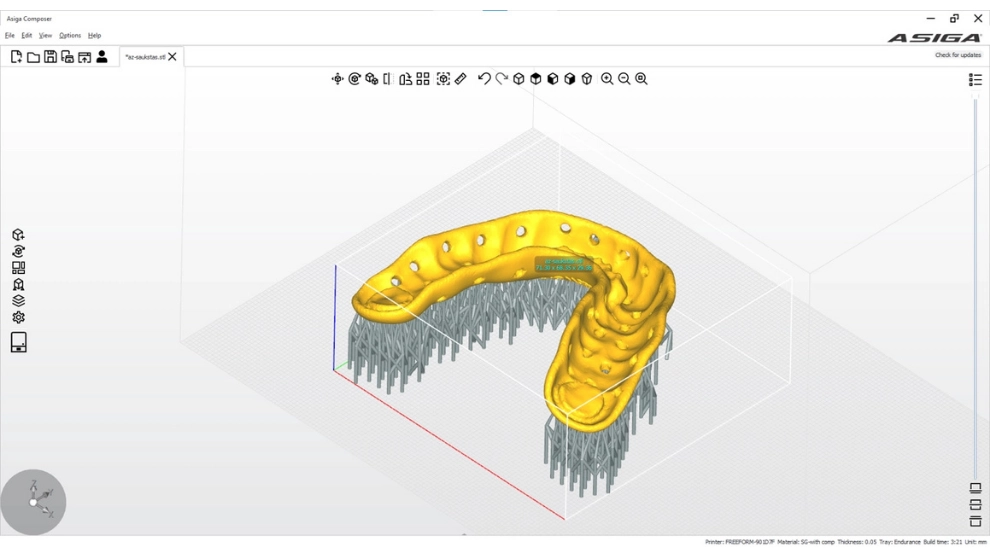
Generate initial support structures using auto-generation feature.
NOTE: As with pre-defined packages user must adjust auto-generated support structures evaluating it based on their expert knowledge.
RECOMMENDATIONS: Always protect critical surfaces from support structures and concentrate them on the perimeter edge of the model. Using this practice allows users to remove support structures from model surface more easily.
The most attention must be paid to parts closest to the building platform, where the highest support density should be. Don’t forget to densify support structures on protruding areas that can encounter failure due to low self-support. For very large parts, it is recommended to add a few thicker support structures, with tip diameter of 0.5 mm, on parts closest to the building platform.
4.5 Prepare the printer and resin
WARNING: When handling any 3D printing resin, make sure you wear nitrile gloves.
WARNING: 3D printing resins can cause damage to your eyes. Always wear protective eyewear when dealing with liquid resins.
WARNING: Make sure you are in well-ventilated area during the 3D printing and post-processing. Ventilation of at least 4 times/hour air exchange is recommended.
WARNING: Always wear appropriate clothing when working with resins to avoid skin contact.
RECOMMENDATION: We highly recommend wearing half facepiece reusable respirator with gas and vapor filters when working with liquid resin and staying in the room with open resin containers.
Prepare your 3D printer by inserting your dedicated CIT-25 resin tray and build platform.
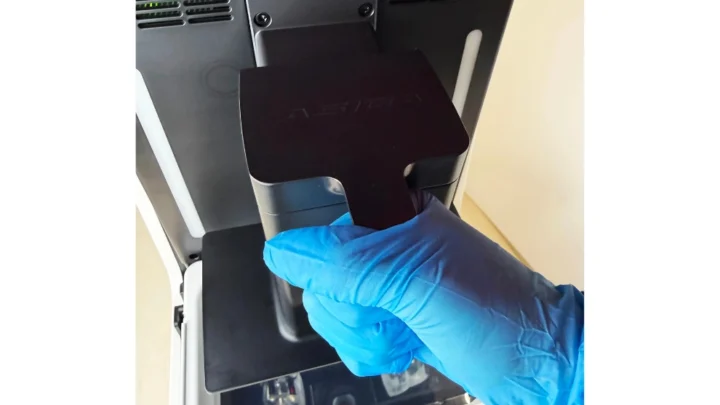
NOTE: Do not forget to use dedicated resin tray and build platform for biocompatible resins.
NOTE: Make sure your printer build platform is well-leveled. Leveling procedure is different for each 3D printer. Contact your printer manufacturer for build platform leveling instructions.
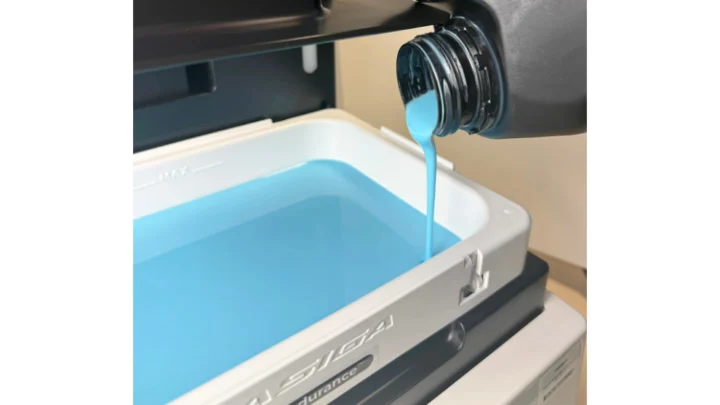
NOTE: Shake the resin bottle thoroughly before pouring it into the resin tray. It is hard to emphasize how critical it is to mix and shake the resin before printing.
Pour the well shaken resin into the resin tray to the desired level. Do not exceed the maximum marker on the resin tray.
4.6 Start print
When you are all set. Send the job to the 3D printer or export it to a memory card and load it to the machine or directly send the file through your network.
NOTE: Be aware of correct ambient temperature during the 3D printing. CIT-25 should be used when it is around 25°C.
5. POST-PROCESSING
Post-processing 3D printed custom impression tray models involves multiple steps, such as removing the part from the build plate, removing supports, rinsing, drying, post-curing and sanding.
5.1 Part removal
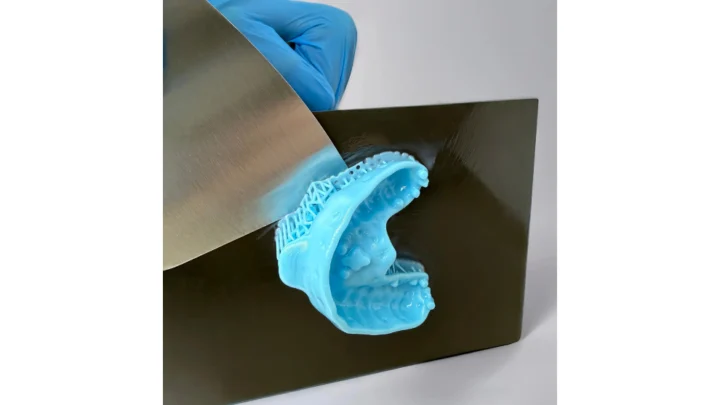
We recommend removing printed parts right after 3D printing and before cleaning, but the part removal can also be done post-cleaning. In order to remove the part from the build platform, first remove platform from the printer. Use a removal tool, such as a metal spatula, and slide it under the base of the printed part.
NOTE: Place the platform on the hard surface while removing the part. It will significantly reduce the likelihood of injury.
NOTE: Use your wrist instead of your hand muscles when removing the part. The wrist has a lot more control capabilities than the entire hand. Moreover, wrist movements have a relatively low amplitude compared to hand movements, which significantly reduces the likelihood of accidental, uncontrolled motions that could cause injury during part removal.
5.2 Remove supports
Support structures can be removed either right after 3D printing, washing, or after post-curing. As post-curing could cause unwanted warpage, existing supports can help preserve the correct geometry and avoid warpage. On the other hand, support removal after post-curing could be more difficult as material becomes harder and relatively more brittle.
5.2.1 Removing supports after printing
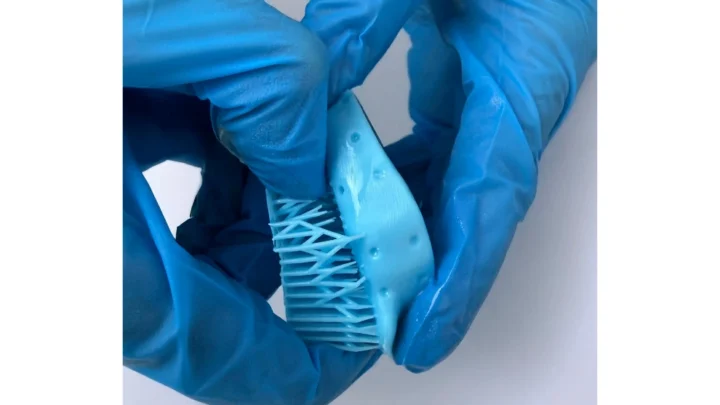
Supports can be removed using flush cutters or similar tools. Cut the supports at touchpoints attached to the custom impression tray model. Material at this point is relatively soft and it is easier to remove supports.
5.2.2 Removing support after post-curing
After cleaning and post-curing supports could be removed using flush cutters or specialized equipment like hand-held disc cutters.
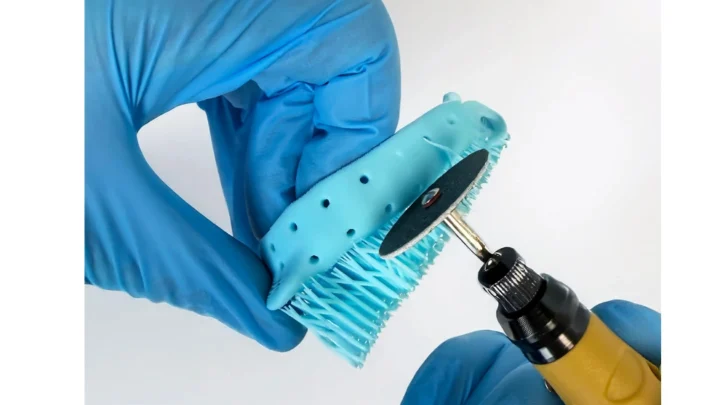
WARNING: Be aware that the material is more brittle and harder after post-curing. Make sure you wear eye protection.
WARNING: Material dust is dangerous. If you use disc cutter or sanding tools, make sure you use suitable respirators or half facepiece reusable respirator with appropriate filters.
Inspect part carefully when removing supports, especially after post-curing. If any kind of cracks or damage is detected, discard the model.
5.3 Part washing in isopropyl alcohol
5.3.1 Washing station
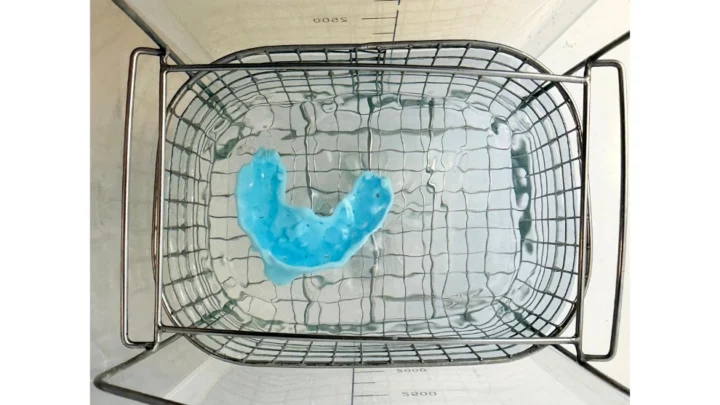
If you do own a washing station with magnetic stirring, put the part into the metal basket and fill container with fresh 99% isopropyl alcohol (IPA). Make sure that the part is fully submerged and check that during cleaning part also stays submerged.
Set the timer to 10 minutes and start cleaning.
NOTE: Use dedicated washing station for biocompatible materials. Do not mix dirty IPA with biocompatible and non-biocompatible materials as that could compromise biocompatibility of printed part.
5.3.2 Ultrasonic cleaner
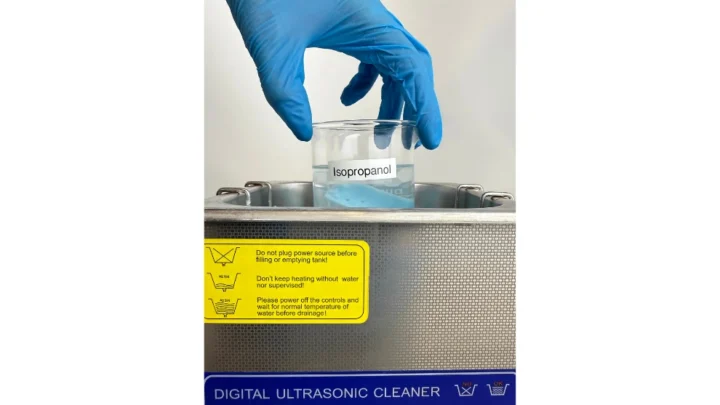
Put the printed part in a plastic (preferably HDPE) container or a glass beaker filled with fresh 99% IPA. Make sure that the part is fully submerged in IPA. Place that container into ultrasonic bath filled with water and run the sonication for 1 minute, swirl it around and sonicate for another 1 minute.
5.3.3 Regular closed containers
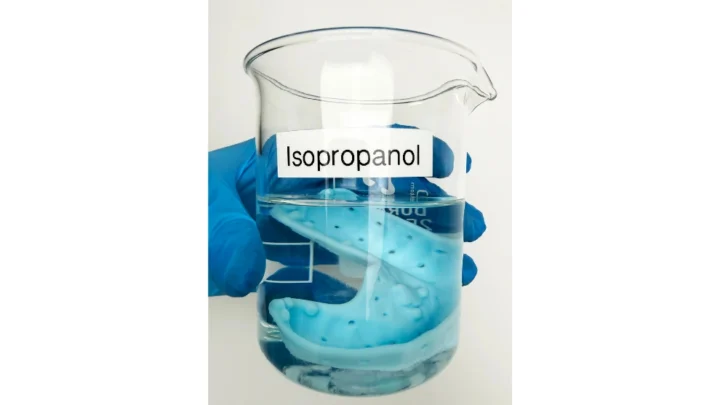
If you do not have automated cleaning equipment, you can clean the part manually using regular sealed plastic (preferably HDPE) containers. Put the part into the container and fill it with fresh 99% IPA, make sure the part is fully submerged in IPA. Follow this procedure:
- Let the part rest in IPA container for 5 minutes.
- Swirl the IPA container with the part in it actively for another 1 minute.
- Leave it still but fully submerged to rest for another 5 minutes after swirling.
- Finally, swirl the bath actively again for 1 minute.
5.4 Part drying
Dry the part with either compressed air or leave it to dry naturally in a well ventilated area for at least 30 minutes. Inspect dry parts very carefully for uncured resin or other particles. You can easily identify uncured resin on a surface of a dry part when it has “wet” stains. Pay special attention to negative features like holes or intricate spots, where resin could still could be trapped.
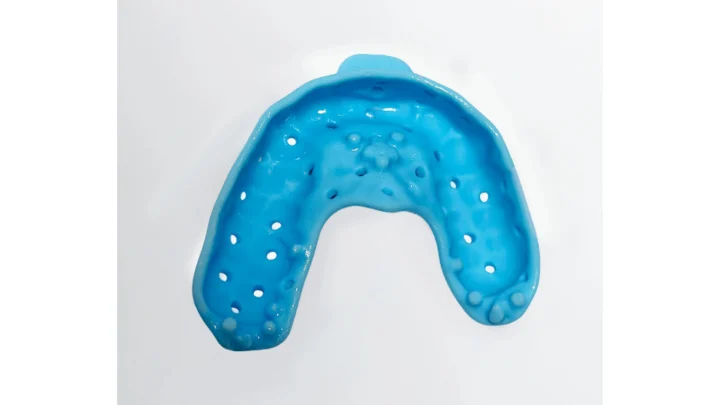
If you find “wet” stains or other particles, you can repeat cleaning cycle again. If secondary cleaning cycle is needed, we recommend changing IPA that you used to a clean one.
5.5 Post-curing
In general, if alginates are used for the impression, post-curing the part in UV chamber with <405nm LEDs for 10 minutes is sufficient. Make sure that all surfaces are post-cured. If your UV chamber does not provide uniform light to the entire surface of the part, after 10 minutes change the position of the part (i.e. turn it upside down) and post-cure again for another 10 minutes.
DISCLAIMER: Color is a response variable. It can vary depending on wavelength of 3D LCD/mSLA or DLP printer that was used to build the tray model, post-curing parameters and natural effects of time.
However, if silicones are used for the impression, then extra curing will be required to make sure the printed tray is fully cured and does not inhibit the curing of silicone. Taking this information into consideration, we recommend sticking to our predefined post curing settings for specific equipment:
| Post-curing machine | Temperature | Atmosphere | Time |
| Asiga Cure | 25 °C | Air | 15 minutes |
| Formlabs Form Cure | 25 °C | Air | 20 minutes |
| Photopol Smart A5408S/D | 25 °C | Air | 15 minutes |
| Anycubic Wash & Cure 3 | 25 °C | Air | 30 minutes |
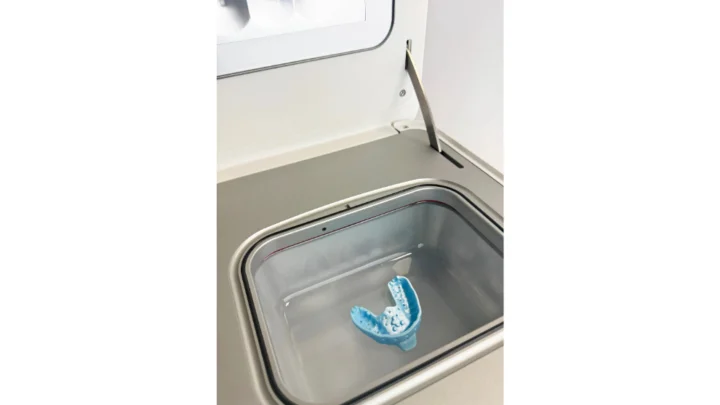
WARNING: Post-curing outside of the recommended settings can result in poor mechanical and biocompatibility properties, moreover, insufficient curing can lead to silicone curing inhibition. Please post-cure only in accordance with official recommendations from AmeraLabs for the best results.
5.6 Support removal
If you have not removed support right after 3D printing, please follow 5.2.2 Removing support after post-curing section for details on how to remove supports.
5.7 Sanding
After support removal left-over marks can be sanded using typical methods such as high grit sandpaper so the maximum comfort to a patient can be ensured.
WARNING: Material dust is dangerous. Make sure you use suitable respirators or a half facepiece reusable respirator with appropriate filters when sanding.
WARNING: Inspect the part carefully for any kind of cracks or damage and if they are detected, discard the model.
6. USE
6.1 Disinfection
The appliances may be cleaned and disinfected according to internal facility protocols. Verified disinfection methods are:
- Soak the finished product in clean and fresh 70% IPA for 5 minutes.
- Soak the finished product in clean and fresh 2% chlorhexidine solution for 2 minutes.
It is important not to leave the part in the disinfection solution for longer than 5 minutes due to possible negative effects. After disinfection, examine the part for damage or cracks to ensure that produced part meets performance requirements.
NOTE: Do not leave custom impression tray models in disinfectant solution for an extended period of time as it may lead to degradation of properties.
IMPORTANT: After disinfection or sterilization, inspect the printed part for cracks and damage to ensure the integrity of the printed part. If any kind of cracks or damage is detected, discard the model.
7. BIOCOMPATIBILITY
CIT-25 resin is non-cytotoxic, not a sensitizer, non-irritating and complies with EN ISO 10993-1.
8. ADDITIONAL DOCUMENTS
Additional documents are available upon request and on our website at https://ameralabs.com/shop/CIT-25/
- EC Declaration of Conformity
- Information For Use
- Technical Data Sheet
- Material Safety Datasheet
9. CONTACT INFORMATION
Manufacturer: MB Labsamera
Draugystės st. 14, LT-51259 Kaunas, Lithuania
support@ameralabs.com